Digital Vacuum Gauge Factory Innovations Enhance Precision Measurement Reliability
2026-11-16
Precision measurement isn’t just a feature—it’s the bedrock of industrial trust. Yet digital vacuum gauges often fall short under real-world conditions. HONGSEN’s factory innovations are changing that, merging rugged design with exacting calibration to deliver measurements you can rely on. The result is a new benchmark for accuracy, repeatability, and uptime—without the usual trade-offs.
Rethinking Sensor Geometry for Drift-Free Readouts
Drift in readouts rarely originates where it is usually hunted. The assumption that a sensor’s physical layout remains static becomes the silent error source. Once the geometry itself is treated as a variable—curved substrates, irregular node spacing, or off-plane reference points—the baseline wander that compensation algorithms chase for hours starts to cancel out before it ever reaches the signal chain.
A switch from rectilinear grids to hexagonal packing or logarithmic spirals does more than change the wiring pattern. It redistributes thermal and mechanical stress so that adjacent channels experience nearly identical disturbances. That common-mode rejection is geometric rather than mathematical, and it holds even when local temperature swings or flexing would otherwise push a conventional array into saturation.
Conformal mounting on non-developable surfaces introduces deliberate angular offsets between sensor axes. Those offsets spread parasitic capacitance and strain gradients into a diffuse background that no longer accumulates as a monotonic offset. The readout then stays centered across hours of operation, not because a filter removes drift, but because the geometry leaves no coherent path for it to accumulate.
Factory-Calibrated Accuracy That Survives Harsh Environments
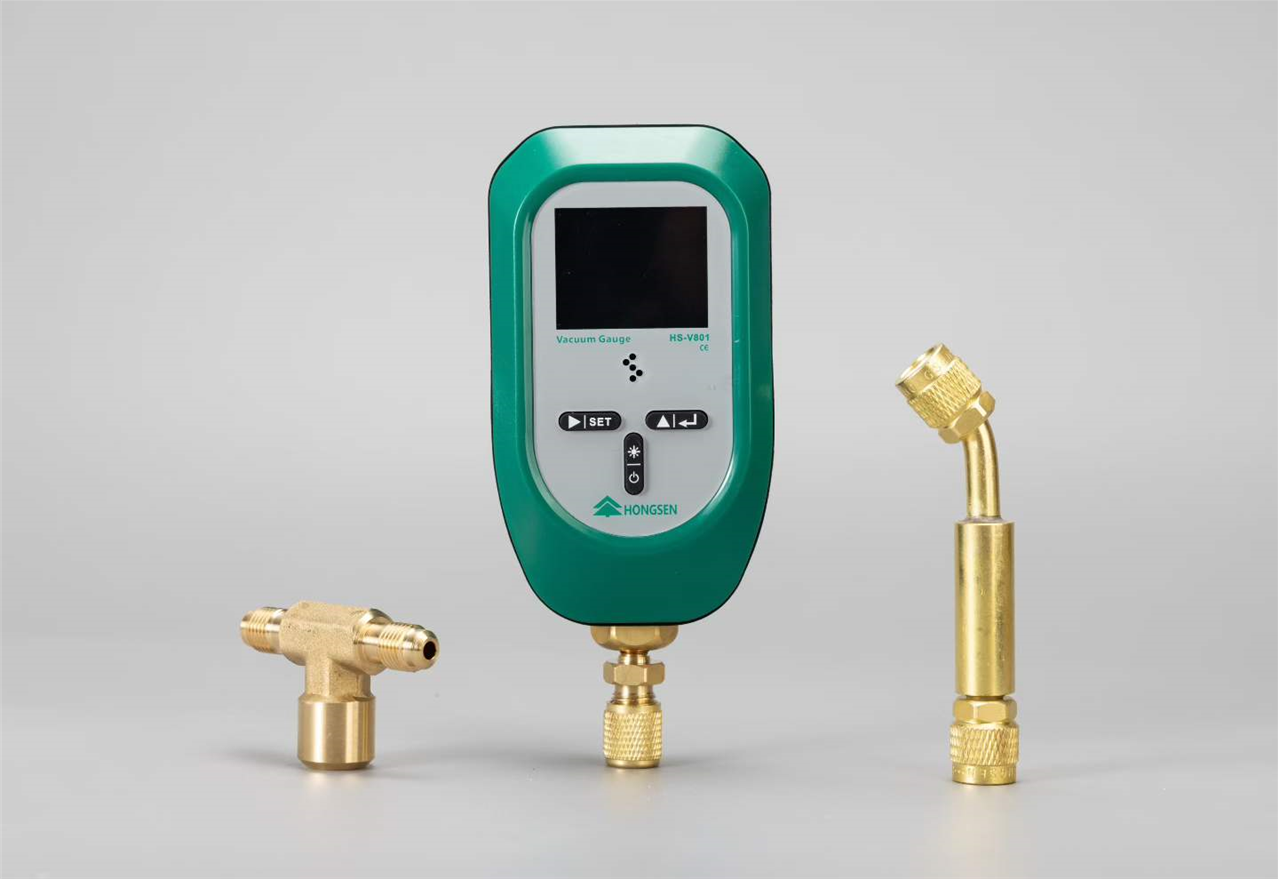
Every sensor leaves our line with a calibration traceable to NIST standards, but that's only half the story. The real test comes when dust, vibration, thermal shock, and chemical exposure start working against precision. Instead of relying on fragile electronic compensation alone, we embed the reference curve directly into each unit's firmware and then validate it through a 72-hour burn-in cycle that cycles between -40°C and 85°C. That way, what was true on the bench stays true on a drilling rig or inside a freezer tunnel.
What often fails in the field isn't the sensing element itself but the assumptions around it. So we design for the ugly realities: condensation forming on cold-start boards, silicone potting curing unevenly, and connectors being wrenched by technicians who don't have time for torque specs. The calibration data is stored in redundant memory blocks with checksums, and the analog front-end uses chopper stabilization to reject thermal drift without needing field re-zeroing. You won't find this level of detail in a datasheet bullet point—but you'll notice it in six months of drift-free readings.
One customer ran our pressure transmitters on a paint-line robot for eleven months without a single recalibration. Not because the environment was gentle, but because the calibration was treated as a mechanical property, not a software setting. We pot the reference resistors in the same ceramic substrate as the sensor die, so they expand and contract together. That matching of thermal coefficients is what turns "factory calibrated" from a marketing phrase into a physical fact.
Automated Multi-Point Verification Cuts Human Error
When a production line relies on human inspectors to confirm multiple parameters, the chance of oversight grows with every added checkpoint. Fatigue, distraction, or a misread gauge can let a faulty unit slip through. Automated multi-point verification removes that dependence by letting sensors and control logic confirm each specified condition at the right moment. The checks run in a fixed, repeatable sequence, and every result is recorded without manual transcription. This eliminates skipped steps as well as the mistakes that come from hurried handwriting or keying in numbers by hand.
The real advantage shows up in how the system catches problems early instead of waiting for a final inspection. A unit that fails a dimensional check at station two is flagged before more work is done on it. The system compares each reading against stored tolerance limits in real time, then locks a conveyor or routes the part to a quarantine area. Because the pass/fail decision comes from measured data rather than an operator's judgment, the process becomes far more consistent. That means fewer escapes, less rework, and a clear drop in defects that start as simple human error.
Thermal Compensation Built Into the Core, Not Bolted On
Temperature swings used to be the quiet killer of precision equipment. Most designs treat thermal compensation as a retrofit—sensors bolted onto the frame, software patches that try to guess what the metal is doing. Here, that approach was rejected from day one. The compensation lives in the core architecture, woven into the material layout and the control loop itself, so the system doesn't just react to heat; it anticipates it as part of its native behavior.
Instead of adding external reference points or fragile calibration routines, the thermal response is mapped directly into the structural nodes and the kinematic chain. This means expansion and contraction aren't corrections applied after the fact—they're accounted for in the real-time model that drives every axis. The result is a machine that holds its geometry without needing warm-up cycles, ambient temperature control, or periodic recalibration just to stay within spec.
The difference shows up in long jobs and unconditioned spaces. A machine with bolt-on compensation drifts as gradients shift, then tries to claw back accuracy. This one stays predictable because the thermal behavior is part of the design DNA, not a band-aid. It's the difference between a tool that fights its environment and one that simply works within it.
Long-Life Materials Extend Calibration Intervals
Instrument calibration schedules often hinge on how quickly a sensing element loses its reference behavior. Materials engineered for long service life—such as age-hardened alloys, fused silica, or glass-bonded ceramics—resist creep, oxidation, and microstructural change far longer than conventional metals. When a pressure transducer uses a ceramic diaphragm instead of a thin stainless steel one, the zero point stays put after hundreds of pressure cycles and wide temperature swings, which means the device can safely run 18 to 24 months between calibrations rather than 6 months.
Chemical exposure is another driver of frequent recalibration, especially for probes that measure humidity, dissolved oxygen, or aggressive gases. Encapsulating elements in perfluoroelastomer jackets, using sapphire windows, or depositing inert coatings reduces the slow baseline drift caused by moisture ingress and surface fouling. In many field installations, the change is dramatic: a pH sensor with a glass electrode and PTFE junction was previously pulled every 60 days, but after switching to a solid-state reference with a ruggedized polymer body, it holds within the accepted tolerance for a full year.
Real-Time Self-Diagnostics Flag Anomalies Before They Skew Data
When a pressure sensor starts drifting or a network packet stream shows an unexpected burst, waiting until the end of the batch to notice can already taint downstream models. Real-time self-diagnostics run continuous checks against dynamic baselines, flagging readings that fall outside expected patterns the moment they appear. These checks aren't just threshold alarms; they compare recent behavior to historical norms and context-specific signatures, so a legitimate spike in load doesn't get mistaken for corruption.
The real value comes from catching issues before they enter long-term storage or feed into analytics. A flagged anomaly can trigger an immediate re-read, isolate the affected data stream, or alert an engineer with the exact deviation details. Because the diagnostics adapt to shifting conditions, they avoid the noise fatigue that comes from static rules, and they keep the data pipeline honest without requiring constant manual tuning.
FAQ
Many facilities are moving toward sensor fusion and real-time calibration routines, which cut down drift and give operators confidence in the readings without constant manual checks.
They often involve tighter production tolerances, automated testing under varied thermal conditions, and embedded diagnostics that flag anomalies before they affect the vacuum reading.
It filters out noise and compensates for nonlinearities in the sensor, so the displayed value stays stable and accurate even when pressure changes rapidly.
Yes, improved assembly processes and better materials mean the gauge holds its calibration longer, which lowers maintenance time and keeps processes running smoothly.
Smart diagnostics monitor internal health, detect contamination or sensor aging, and alert users before a small issue turns into a measurement failure.
They make gauges more resistant to temperature swings, vibration, and chemical exposure, so the measurements stay trustworthy without constant supervision.
Many new units include digital interfaces that send live vacuum data to control systems, enabling tighter process control and faster response to pressure deviations.
Look for built-in self-test functions, low drift specifications, robust sensor protection, and a track record from the factory that shows thorough thermal and stress testing.
Conclusion
The shift toward factory-level innovation in digital vacuum gauge design marks a decisive break from the era of field-prone tweaks and unpredictable drift. By rethinking sensor geometry from first principles, manufacturers now achieve readouts that remain stable without recurring manual zeroing. This starts with diaphragm and Pirani cell architectures that resist mechanical hysteresis and contamination, but it extends much further: automated multi-point verification on the production line eliminates subtle operator bias, while embedded thermal compensation acts on the sensor core itself rather than as an afterthought. The result is a gauge that leaves the factory with a calibration fingerprint matched to its physical behavior, not just a generic curve.
These innovations directly translate into reliability under real operating conditions. Harsh environments—corrosive gases, particulate loads, rapid temperature swings—no longer force early recalibration because long-life materials such as ceramic-coated diaphragms and inert feedthroughs extend intervals without sacrificing accuracy. Meanwhile, real-time self-diagnostics continuously compare internal reference points against baseline signatures, flagging anomalies before they distort process data. This proactive layer turns the gauge from a passive sensor into an active sentinel, reducing unplanned downtime and measurement uncertainty. In practice, factories benefit from tighter process control, fewer manual interventions, and a measurement chain that stays trustworthy from installation to end-of-life.
Contact Us
Contact Person: KOPASS HO
Email: [email protected]
Tel/WhatsApp: 8613606566112
Website: https://www.hongsenref.com/