PTFE Envelope Gasket Supplier Evaluation Checklist for Engineers
2026-11-16
PTFE envelope gaskets are only as reliable as the supplier behind them—yet too many engineers learn that the hard way after a seal fails in the field. Before you settle for another round of sample testing and supplier promises, run through this evaluation checklist. TAIFNO has seen firsthand what separates a consistent gasket maker from a costly gamble, and this guide breaks down the exact criteria you should be screening for.
Beyond the Spec Sheet: Confirming True Virgin PTFE Content
A data sheet can list 'virgin PTFE' while the actual resin blend includes reprocessed scrap or cheaper fillers that compromise chemical resistance and surface finish. Without independent verification, you are trusting a label rather than the material itself. The only reliable way to confirm true virgin content is through thermal analysis combined with trace element screening, because regrind and recycled PTFE leave behind measurable signatures in melt flow behavior and residual contamination.
Differential scanning calorimetry reveals the crystallization temperature and heat of fusion, which shift when even 5–10% reprocessed PTFE is mixed into virgin resin. Pair that with a simple ash test or X-ray fluorescence scan to detect metallic traces from processing equipment or unintended additives. Suppliers who hesitate to share raw resin certificates or batch-level test data are often blending something they should not be.
Ultimately, confirming true virgin PTFE means going beyond the marketing language and asking for physical evidence tied to the exact lot you receive. A reputable source will welcome a third-party audit of their incoming resin, while a supplier pushing only a glossy brochure rarely has anything worth hiding.
Envelope Fusion Quality You Can Actually Inspect Before Ordering
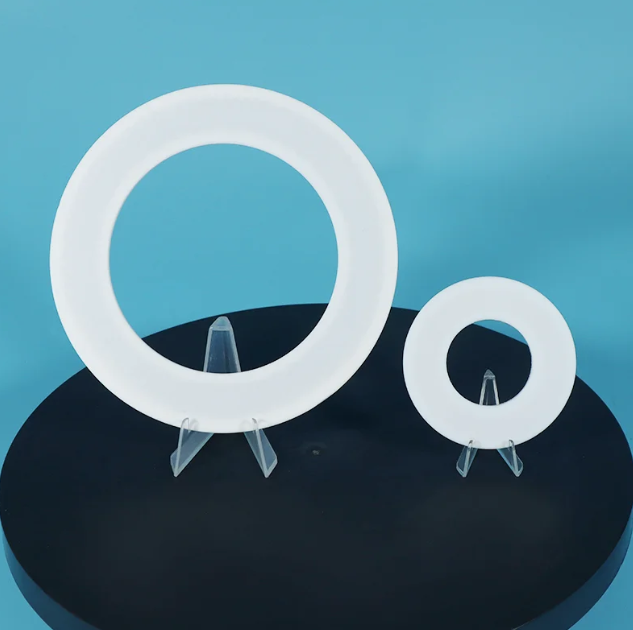
Most suppliers ask you to trust a spec sheet until the cartons show up. Not here. You can request a physical sample set or watch close-up video of the envelope fusion zone before committing to a single production run. Check the glue penetration, the fiber tear pattern, and how the flap behaves under repeated flexing—all before the order is placed.
That early inspection window catches the issues that usually surface weeks later: uneven adhesive lines, weak corners, or a seam that looks fine in photos but fails in your mailroom. Instead of hoping for the best, you sign off on the exact fusion quality you will receive. No surprises, no rework debates, just a bonded edge that holds up from insertion to final delivery.
Tolerances That Survive Real Flange Misalignment
Flange connections rarely sit perfectly square in the field. Pipe rack sag, thermal growth, foundation settling, and human error during fit-up all push mating faces out of alignment by degrees that never appear on the drawing. A tolerance that looks generous on paper—say, ±0.5 mm of radial offset—can vanish the moment a bolting crew uses a come-along to pull two misaligned spools together. Surviving real misalignment means designing for the gap between theoretical geometry and what actually happens when steel meets steel under tension.
One practical approach is to stop relying on flat-face contact as the primary sealing mechanism. Spherical washers, self-aligning gaskets, and flanges with a slight convex-to-concave interface absorb angular deviation without concentrating stress at the bolt holes. For radial offset, oversizing bolt holes or using slotted connections buys back a few millimeters of forgiveness, but every extra millimeter also increases the chance of gasket blowout if the clamping load becomes uneven. The trick is to pair these features with controlled bolting sequences that pull the joint into alignment gradually rather than forcing it all at once.
Validation matters more than the number stamped on the flange. A tolerance that survives one misalignment condition may fail under combined loading—say, 2° of angular tilt plus 3 mm of offset plus internal pressure cycling. Running a few physical assembly tests with deliberately skewed flanges, or using nonlinear finite element analysis to map gasket stress across the seating surface, reveals where the real safety margin lies. In many cases, a tighter geometric tolerance on paper gives less field reliability than a looser one paired with a more forgiving joint design.
Batch-to-Batch Uniformity Without Relying on Supplier Claims
In practice, the only way to confirm that incoming raw materials meet your formulation's performance envelope is to run your own orthogonal assays. A supplier's certificate of analysis may look clean, but it seldom reflects how a given lot behaves under your specific processing conditions—shear history, pH shifts, or thermal cycling can expose hidden variability that a standard specification sheet never captures. By establishing internal lot-acceptance tests that directly tie to critical quality attributes, you create a feedback loop that catches drift before it reaches production.
One effective approach is to build a small reference library of previously accepted lots, then fingerprint each new arrival against that set using a method you can execute quickly on the floor. This might be a simple rotational rheology scan, a particle-size distribution curve, or a near-infrared spectrum—whatever is most sensitive to the failure modes you have actually seen. Over time, the data accumulate into a practical model of what normal variation looks like, so an outlier becomes obvious without waiting for a full QC panel.
The payoff is not just fewer rejected batches; it is the confidence to push back on supplier substitutions or process changes with numbers you generated yourself. When a vendor quietly shifts feedstock sources or tweaks a manufacturing step, internal uniformity data often flag the shift before a formal specification is breached. That proactive stance turns batch-to-batch control from a paperwork exercise into a real manufacturing advantage.
Cleanroom Handling Proof for Critical Media Service
Every critical media component passes through a tightly controlled cleanroom environment the moment it enters our facility. We track particle counts, air pressure differentials, and surface cleanliness at scheduled intervals, not just as a formality but because even a single stray fiber can compromise downstream performance. Operators follow documented gowning and material transfer procedures, and each step is logged against a lot-specific record so the handling history stays fully traceable.
To back up our cleanroom claims, we provide objective proof rather than relying on internal statements alone. Third-party audits, real-time monitoring data, and periodic microbial and particulate sampling are compiled into a handling evidence package for critical media lots. This includes wipe tests, settle plate results, and any out-of-specification events with corrective actions taken, giving quality teams the confidence to approve materials without re-testing everything from scratch.
What sets our approach apart is that cleanroom handling proof is embedded into the service workflow instead of treated as a separate document request. When you receive a critical media shipment, the accompanying record shows exactly which operator handled it, under which cleanroom classification, and at what time. That level of granularity removes guesswork during audits and makes the entire chain of custody transparent from incoming inspection to final packaging.
Creep Relaxation Data That Predicts Leak-Free Years
Creep relaxation data often gets overlooked because it doesn't show immediate failure. Yet this slow, silent material behavior is precisely what separates a connection that leaks within months from one that stays tight for decades. By recording how much preload is lost over time at a given temperature, engineers can map out a realistic lifetime curve instead of relying on short-term torque checks.
The real value emerges when you stop treating gasket and bolt materials as static. A properly designed test program captures the drop in load after minutes, hours, and thousands of hours, then fits that decay to a logarithmic or power-law model. Once you have the curve, it's straightforward to calculate the remaining clamp force after five, ten, or twenty years. In many cases, that remaining force is still above the threshold needed to prevent leakage, which gives you confidence without guesswork.
Field data backs this up. Flanges that leak prematurely usually show an early and steep relaxation trend, visible within the first few hundred hours of testing. Conversely, systems that hold their preload beyond the first plateau tend to stay reliable for their entire service life. Publishing and comparing these curves for different gasket types and bolt grades lets designers pick materials that won't quietly let go after a decade of thermal cycling.
FAQ
Ask for the exact PTFE resin grade, filler type and percentage if any, plus independent chemical resistance data for your media at operating temperature. A supplier should also furnish certificates showing compliance with FDA 21 CFR 177.1550 or USP Class VI when clean service is involved, along with an EN 10204 3.1 material certificate tracing the lot.
Request first-article inspection reports with actual measured values for inner diameter, outer diameter, envelope thickness, and flange sealing face flatness. These should come from a calibrated CMM or optical comparator, not a hand caliper. Compare the reported scatter against your piping flange standard, such as ASME B16.21, to see if the supplier holds tighter than the minimum allowed tolerance.
Look for equipment that can run leak-tightness tests under your service conditions, such as a helium mass spectrometer or a DIN 3535 gas leak rig. Facilities with their own tensile and elongation testing per ASTM D4894 or D4895, plus a hardness tester and a sintering oven with temperature profiling, are usually controlling the process rather than just buying and reselling.
Observe whether the PTFE resin is stored in a clean, dry area and whether the sintering ovens have validated temperature curves with alarms. Check if the envelope is folded or welded with consistent overlap and no pin holes, and ask to see how the manufacturer prevents contamination between white PTFE and graphite-filled grades in shared tooling.
Ask for thermal cycling test data, not just a single-temperature rating. A credible supplier will have run the gasket through repeated cycles between your minimum and maximum expected temperatures while monitoring relaxation and leak rate. You can also request comparative compression set data from PTFE samples aged at elevated temperature to see whether the envelope will remain elastic enough to follow flange movement.
A reliable supplier stamps or laser-marks each gasket with a batch number that links back to the raw PTFE resin lot, sintering cycle log, and final inspection record. They should retain samples from each production run for a defined period and be able to retrieve those records within a day if a failure investigation is needed. Transactional vendors often cannot tell you which resin lot went into which gasket.
For general chemical service, look for compliance with FDA 21 CFR 177.1550 for the PTFE material, USP Class VI when the gasket contacts pharmaceuticals, and a declaration of conformity to the Pressure Equipment Directive if the gasket is used in EU pressure systems. For German or TA-Luft applications, ask for a TA-Luft leak-tightness certificate from an independent test lab. Also check whether the supplier holds ISO 9001 with a scope that explicitly covers gasket manufacturing, not just distribution.
Request gasket compression and recovery curves measured at multiple stress levels and temperatures, plus long-term creep relaxation data from a test like EN 13555. Compare the supplier’s envelope wall thickness, overlap construction, and filler type against known reference gaskets that have performed well in similar flanges. A vendor that only provides a generic pressure-temperature chart without any measured elastic recovery data is often guessing at long-term behavior.
Conclusion
When vetting a PTFE envelope gasket supplier, engineers quickly learn that a polished datasheet rarely tells the whole story. The first hurdle is verifying true virgin PTFE content, not a reprocessed blend that hides fillers or compromises chemical resistance. Ask for raw material certifications and even test samples with a simple specific gravity check—reprocessed grades often fall outside the expected 2.13–2.20 range. Equally important is envelope fusion quality. You cannot rely on a supplier's word that the seam is pinhole-free; request cross-sectioned samples or insist on a clear inspection protocol before ordering. A fused seam that shows a crisp, uniform melt line without gaps or charring is a good sign, while wavy or fractured joints predict early leakage. Without this hands-on verification, you are gambling on a barrier that may fail the moment aggressive media hits a tiny void.
Beyond chemistry and fusion, real-world flange conditions demand tolerances that survive misalignment. Standard gaskets with tight cut dimensions often buckle or wrinkle when flanges are slightly offset or unevenly torqued. A supplier should provide tolerance data based on actual compression tests across varied bolt loads, not just ideal flat surfaces. Batch-to-batch uniformity is another silent killer: ask for SPC charts or, better yet, request a lot-by-lot FTIR or DSC scan to confirm the PTFE crystalline structure hasn't drifted. For critical media service, cleanroom handling proof matters—look for particle count certificates or evidence of ISO Class 7+ packaging, because even microscopic debris can contaminate a sterile line. Finally, demand creep relaxation data that goes beyond a 24-hour lab test. Predictive curves at your operating temperature and stress range tell you whether the gasket will maintain sealing force after years of thermal cycling. Suppliers who cannot produce this long-term dataset are likely hiding a material that will quietly lose spring-back and invite a leak when no one is watching.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com