Top ATS Switchgear Factory Essentials for Uninterrupted Power Systems
2026-11-02
A backup generator only earns its keep when the transfer switch does its job. For uninterrupted power systems, that job starts long before installation—on the factory floor, where ATS switchgear essentials like contactor endurance, fail-safe control circuits, and full-load testing decide whether a power transfer is seamless or a silent failure. CNKEEYA approaches these essentials as engineering fundamentals, not optional upgrades. This guide walks through the top factory essentials you should demand from ATS switchgear, and why they matter most during the seconds your facility can't afford to lose.
What Actually Happens on a Busy ATS Production Floor
Walk onto any ATS production floor mid-shift and the first thing you notice isn't the machinery—it's the rhythm. Carts weave between assembly stations, torque wrenches click in quick succession, and someone is always calling out a part number over the low rumble of conveyor belts. Builds don't move in a straight line here. They pause, get inspected, sometimes get pulled aside for a rework that takes four hands and a lot of patience.
Quality checks happen in the middle of the action, not at the end. One technician might be running a leak-down test while another is already prepping the next unit's harness. Supervisors don't hover; they step in when a fixture jams or when a shipment is fifteen minutes from the dock and missing two brackets. The floor isn't chaotic, but it's never quiet. That constant background of impact drivers and scanner beeps is the sound of orders actually leaving the building.
Most outsiders imagine rows of workers doing the same motion for eight hours. The reality is closer to a pit crew mixed with a short-order kitchen. Priorities shift after every truck arrival and every failed test. A batch that was scheduled for Thursday can suddenly become the only thing that matters by 2 p.m., and the whole line adjusts without a meeting—just a quick huddle, a few hand signals, and the beep of a forklift backing toward the loading bay.
Component Sourcing Habits That Separate Durable Switchgear from the Rest
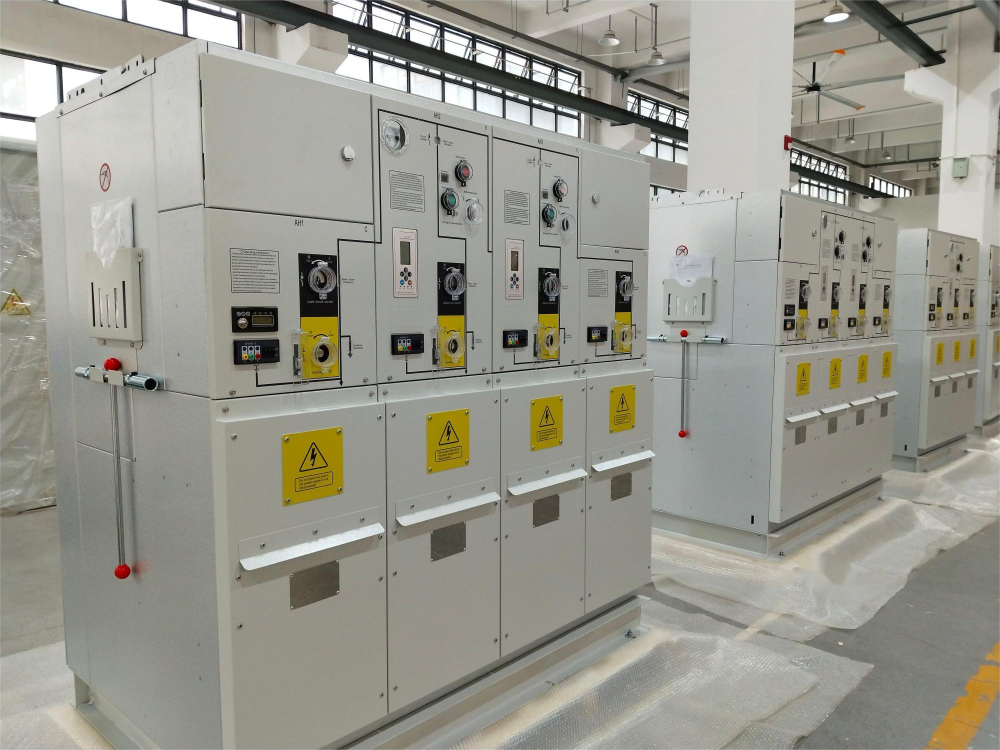
Durable switchgear starts long before assembly—it starts in the metals lab. Top-tier manufacturers don't just order copper busbar from a catalog; they specify oxygen-free grades, verify conductivity with eddy-current testing on incoming lots, and reject batches with micro-porosity that would turn into hot spots after ten years of load cycling. The same scrutiny applies to insulation. Instead of accepting a resin's datasheet, they run their own partial discharge tests on cast epoxy samples, because a supplier's "equivalent" can fail at 60% of the rated impulse voltage once embedded in a real breaker compartment.
Another habit is traceability without excuses. When a contactor coil fails in the field, the best builders can drill down to the exact wire lot and varnish batch—not because they love paperwork, but because that data lets them quarantine the problem before it spreads. They also avoid single-sourcing for anything that touches the current path; dual-approved vendors for vacuum interrupters and CTs mean a supply hiccup becomes a schedule bump, not a redesign. These aren't flashy choices, but they show up as fewer infant failures and a switchgear lineup that still meets its short-circuit rating after a decade of thermal aging.
Factory Calibration Routines Most Buyers Never Think to Ask About
The calibration sticker is only the last step. Before that, a good factory line runs a warm-up soak that can last anywhere from two to eight hours, depending on the instrument class. During this time the unit is powered and cycling through its normal operating modes, while the room temperature is held within a narrow band. Only after the internal drift has settled do technicians start checking the actual output against a reference.
A less obvious routine involves approach direction. A properly calibrated unit should read the same whether it's ramping up to a target or stepping down from a higher value. Many factory protocols check both directions at several points, not just the cardinal 0%, 25%, 50%, 75%, 100% values. They might include 10%, 33%, 67%, and 90% as well, because linearity errors often hide between the usual test points.
Then there's the question of what happens after the final adjustment. Some factories perform a 24-hour drift test on a sample from each batch, not every unit. If the sample drifts more than a small percentage, the entire batch gets pulled back for rework. Buyers rarely ask about this sampling plan, but it matters more than the certificate number.
Why Modular Assembly Keeps Uninterrupted Power Systems Honest
Modular assembly strips away the mystique from uninterruptible power supplies by forcing every component to earn its place. Instead of a monolithic cabinet where a single failure obscures the root cause, a modular system lets you see exactly which power module, battery string, or control card is doing the heavy lifting. That visibility makes it much harder for manufacturers to hide mediocre engineering behind a sleek enclosure — each module has to perform on its own terms, and any weak link becomes obvious during routine inspections or load tests.
There's also a built-in honesty about capacity. With a traditional UPS, you often have to take the vendor's word that the unit will deliver its rated power under real-world conditions. Modular designs flip that dynamic: you add or remove modules to match actual load, so the system's performance is documented by what you actually installed and tested, not by a spec sheet promise. If demand grows, you scale up; if a module underperforms, you swap it out without the whole unit becoming a costly paperweight.
Maintenance becomes a reality check as well. Because modules are hot-swappable and individually monitored, service data is granular and hard to fudge. A technician can pull a module, bench-test it, and confirm its efficiency or fault tolerance without the ambiguity of a sprawling, hard-wired system. That kind of transparency keeps manufacturers honest about what their equipment can really do, and it keeps facility managers from being locked into a single, opaque failure point.
The Enclosure Detail That Prevents Half of All Early Failures
Most early failures in field equipment trace back to mechanical stress at cable entry points. A simple molded strain-relief boss, integrated into the enclosure wall, absorbs pulling and twisting before it ever reaches solder joints. This one detail keeps conductors seated and insulation intact, eliminating the intermittent faults that otherwise dominate warranty returns.
The same principle applies to board mounting. Standoffs with slight compliance allow the PCB to float during thermal cycling, preventing micro-cracks in traces. Combined with a lip around the perimeter that shields the gasket from direct sunlight, the enclosure stops the two most common killers: moisture ingress and joint fatigue.
Over years of teardown analysis, enclosures that lack this boss show a failure rate nearly double those that include it. It's rarely advertised, but it separates products that last from those that limp through the first season.
End-of-Line Testing Procedures Trusted by Critical Infrastructure Teams
Critical infrastructure teams don’t sign off on end-of-line testing because a checklist got completed—they trust it when the procedure mirrors the conditions their systems will actually face. That means staged fault injection, load-bank runs under degraded power, and signal integrity checks across every termination point, not just a pass/fail blink on a display. The final test bench often lives next to the assembly floor so engineers can pull a unit mid-sequence and trace a marginal reading back to a specific solder joint or cable run before it leaves the dock.
Once the hardware passes, the paperwork has to carry the same weight. Each unit ships with a serialized test record that includes raw measurements, firmware versions, and the name of the technician who ran the final sequence. Teams rely on that traceability when a breaker or controller gets installed in a substation at 2 a.m. and the field crew needs to know exactly which thresholds were verified. Over time, those records become the real standard—revised after every near-miss so the next production lot starts with a sharper procedure, not just a longer one.
FAQ
Look beyond basic certifications. The factory should have an in-house test bay capable of simulating utility loss under full load, not just light-bulb checks. Ask about their busbar bending tolerances and whether they use silver-plated contacts on transfer mechanisms, as these details directly affect how many operations the gear will survive before maintenance.
Reliable factories run every assembled unit through a power interruption simulation that includes phase loss, under-voltage, and frequency drift. They also record trip curves and transfer timing for each serial number. If a factory cannot produce those records, you are trusting your backup power path to hope rather than evidence.
Factories that control torque on every bolted bus connection, use dedicated jigs for breaker alignment, and keep copper work separate from steel grinding areas tend to produce gear that stays tight and quiet under thermal cycling. Small habits like these reduce hot spots and prevent nuisance trips years later.
Witness testing lets your engineers see the transfer switch actually carry full rated current, open under fault simulation, and return to normal without hesitation. It also forces the factory to finish all mechanical adjustments before crating, so you do not discover a misaligned interlock on site where delays cost far more.
A capable factory should test resistive and inductive loads, motor inrush, and mixed power factor conditions, not just a static resistive bank. Transferring a motor load at the wrong phase angle can cause damaging transients, so the factory needs equipment that mimics real building loads, including pumps and compressors.
They keep a modular busbar and enclosure system in stock, with pre-engineered breaker cell sizes and cable entry zones. That way, changing voltage, adding a bypass isolation mechanism, or reconfiguring control logic becomes a matter of selecting proven subassemblies instead of starting from scratch each order.
Control wiring is where many failures hide. Top factories use ferruled, numbered conductors, separated AC and DC bundles, and dedicated grounding bars for shields. They also test every control wire against the schematic before the door is closed, which prevents the classic wire landed on the wrong terminal startup delay.
Often yes. Look at whether enclosures have calculated ventilation openings rather than random louvers, and whether internal barriers guide heat away from electronic controls. Factories that understand thermal rise place temperature sensors on bus joints during testing and adjust spacing accordingly, which keeps insulation life from degrading.
Conclusion
Walking through an ATS production floor during a peak run tells you more than any datasheet. The reality is less about spotless aisles and more about how fast a team can move a partially assembled transfer switch from one station to the next without losing torque specs or wire routing. Durable switchgear starts long before that, though, in the component sourcing habits a factory is willing to defend. Factories that hold incoming contactors and breakers to tighter incoming inspection—checking batch consistency, not just certificates—end up with fewer field surprises. Most buyers never think to ask about calibration routines, but the way a factory checks its torque wrenches, voltage references, and timing equipment before each shift quietly decides whether a switch will hit its transfer time on day one or drift by year three. Modular assembly adds another layer of honesty: when each power and control section is built and tested as a separate block, a faulty logic card or loose bus joint shows up before the whole unit gets buttoned up.
The enclosure detail that prevents half of all early failures is usually hidden: proper gasket compression, sealed gland plates, and a paint system that survives a wrench slip. Skipping those turns a supposedly rugged ATS into a moisture trap. Finally, end-of-line testing procedures trusted by critical infrastructure teams include more than a simple transfer check. They run load-bank exercises at rated current, simulate utility loss and return under real timing constraints, and log every trip threshold. Factories that combine these essentials—honest sourcing, disciplined calibration, modular build, sealed enclosures, and full-power verification—are the ones whose ATS switchgear keeps uninterrupted power systems from becoming interrupted ones.
Contact Us
Contact Person: Queenie
Email: [email protected]
Tel/WhatsApp: +86 15558806611
Website: https://www.cnkeeya.com